Welding and Gas

Ahlsell's range of tools and machines includes power tools, hand tools, plumbing tools, hand, torch and flashlights, measuring and marking tools, cutters, grinding and brushes, brushes, rollers, wallpaper, and painting tools, cutting tools, welding and gas, compressed air, hydraulics, pneumatics, rubber cloths and vibration damping, cleaning tools, property and office, tools and garden products. We value reliable products that last a long time. That is why you will find tools and machines of high quality in our range. Explore all our tools and machines online or in one of our stores.

Products (512)
Electrode ESAB OK 68.82 VacPac
ESAB
Electrode ESAB OK 68.82 VacPac
Art. no.: 388956
OK 68.82 is a high-alloy electrode designed for the joint welding of difficult-to-weld dissimilar steels, surfacing of sliding surfaces, and as a buffer layer for hard-surfacing materials. The distinguishing features of the weld metal include high strength, crack resistance, and wear resistance. The electrode withstands dilution and alloying, delivering high-strength welds in both high-alloy and low-alloy steels and during the joining of widely dissimilar steels. The high chromium content provides a low friction coefficient and scaling resistance up to 115 °C. Welding at an elevated working temperature can often be eliminated except for steels with a high carbon equivalent, where preheating around 150-200 °C should be applied. OK 68.82 truly earns its name as a universal electrode for difficult welding situations in both common and challenging unusual steels. Suitable applications include rollers, forging tools, hot forming tools, punch dies for plastics, etc. OK 68.82 features a highly alloyed core wire, which provides excellent welding properties.
Electrode esab ok 63.20
ESAB
Electrode esab ok 63.20
Art. no.: 116506
OK 63.20 is an extra low-carbon content stainless electrode of type 18Cr 12Ni 2,8Mo primarily intended for position welding of thin-walled pipes. The electrode has a thin casing and can be welded according to the so-called “drop weld method" or vertically descending, which goes quicker. This requires an electrode with very good ignition and re-ignition properties, which makes OK 63.20 very suitable. The electrode is directly suited for the stainless steels types 316 and 316L, for example X3CrNiMo17-13-3 (SS2343), X2CrNiMo18-14-3 (SS2353) or equivalent steels according to other standards. The weld’s low carbon content creates good resistance to inter-crystalline corrosion, but also against spot corrosion and most types of corrosion in reducing and neutral solutions. OK 63.20 can also be used for welding stabilising steel if these will not operate in temperatures exceeding 400°C. Current type DC+, AC OCV 50 V.
Code in accordance with: EN 1600 E 19 12 3 L R 1 1. SFA/AWS A5.4 E316L-16. Werkstoff No. 1.4430. CSA W48 E316L-16.
Approval: CWB CSA W48 - Sepros UNA 409820 - VdTÜV 09716 - CE EN 13479.
Electrode esab ok 61.30
ESAB
Electrode esab ok 61.30
Art. no.: 119422
OK 61.30 is an extra low-carbon stainless all-current electrode made of alloy type 19 Cr 10 Ni. The electrode is intended for welding of austenitic stainless steel equivalent to 304, 304L, 308, 308L, X10CrNi18-8 (SS2331), X5CrNi18-10 (SS2332), SS2333, X2CrNi18-9 (SS2352) or equivalent steel in accordance with other norms. OK 61.30 can also be used for welding stabilising steel X6CrNiTi18-10 (SS2337) and X6CrNiNb18-10 (SS2338) if these will not operate in temperatures exceeding 350°C. OK 61.30 ignites and re-ignites very easily and is very short-circuit proof while welding. The electrode provides beautiful strands and the slag is self-loosening. Fragile dimensions up to 3.2 mm can be welded in all positions.
Current type: DC+, AC OCV 50 V.
Code in accordance with: EN 1600, E 19 9 L R 1 2. SFA/AWS A5.4, E308L-17, Werkstoff No. 1.4316. CSA W48, E 308L-17.
Approval: ABS Stainless - CWB CSA W48 - DB 30.039.02 - DNV 308L - Sepros UNA 409820 - VdTÜV 00792 - CE EN 13479.
Tungsten Electrode RIMAC
Art. no.: 79362229
TIG electrodes are intended for use in Tungsten Gas Arc Welding, a technique used to create precision welds in various industries, including manufacturing, automotive repair, and pipe welding. These electrodes act as conductors of electric current and generate an arc between the electrode and the workpiece. This allows the metal to melt and form strong, precise weld joints.

Significance of Colors:

Within the range of TIG electrodes, you will find different colors, each with a specific meaning and use. Here's a brief overview of the colors:

- Red (DC) – WTh20 (2% Thorium Oxide): The red electrode contains thorium and is very popular for DC welding of steel and stainless steel. It provides a stable arc and long lifespan, but is slightly radioactive.

- White (AC) – WZr8 (.8% Zirconium Oxide): The white electrode is mainly used for AC welding, especially of aluminum. It is stable and resistant to contamination.

- Gold (AC/DC) – WLa20 (2% Lanthanum Oxide): The gold electrode is a versatile all-round electrode that works well for both AC and DC. It has a long lifespan and stable arc.

- Green (AC) – WP (Pure Tungsten): The green electrode consists of 99.5% pure tungsten. Primarily used for AC welding of aluminum and magnesium. It is inexpensive but wears down quickly.

- Blue (AC/DC) – WLa10 (1% Lanthanum Oxide): The blue electrode is good for both AC and DC. It provides a stable arc and is a good alternative to thoriated electrodes without radioactivity.

- Gray (AC/DC) – WCe20 (2% Cerium Oxide): The gray electrode is ideal for low current applications and provides easy ignition. Suitable for both AC and DC, especially for thinner materials.

- Black (AC/DC) – WLa15 (1.5% Lanthanum Oxide): The black electrode provides a stable arc and long lifespan. Good for both AC and DC, especially in automated welding.

- Purple (AC/DC) – WR2 (Mixed Rare Earth Metals): The purple electrode contains a mix of oxides (e.g., lanthanum, cerium, yttrium) and is very stable and versatile. Suitable for both AC and DC.

- Turquoise (AC/DC): Turquoise TIG electrodes contain a blend of oxides and provide a stable arc in AC welding and are used for exotic metals.

No matter your welding application, we have the right TIG electrode for you. Our range is carefully designed to meet the highest performance and quality standards, and the color coding makes it easy to choose the right electrode for your project.

TIG electrodes are crucial for achieving excellent results in Tungsten Gas Arc Welding, and our multicolored collection gives you the option to choose the perfect electrode for your specific application. Whether you are welding aluminum, stainless steel, copper, or other metals, we have the right TIG electrode to make your work smooth and efficient.
Tungsten Electrode RIMACTungsten Electrode RIMACTungsten Electrode RIMACTungsten Electrode RIMACTungsten Electrode RIMAC
+
14
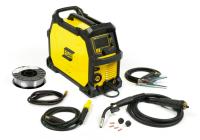
Universal Sweater Esab Rebel EMP215IC KIT
ESAB
Universal Sweater Esab Rebel EMP215IC KIT
Art. no.: 469362
Rebel ™ is developed for MIG/MAG welding with solid wire and wire, electrode welding (MMA) and TIG welding with Lift TIG start. Reel is connected to 1-phase 230V mains voltage. With a groundbreaking design inspired by professional welders, Rebel is the complete package for welding anything - construction steel, aluminium, stainless steel -anywhere.
Application areas: Installation and Assembly, Repair and Maintenance, Garages, Automotive, Lighting Manufacturing and Construction Industry, Agriculture and Welding Training.
MIG output 25%, duty factor: 205A/24. 3V
MMA output 25%, duty factor: 180A/27.2 V
TIG output 30%, duty factor: 180A/17.2 V
Supplied with:
- 3m long ergonomic MXL 200 welding gun with Euro connector.
- 3m welding and return cables with MP 200 clamp and Handy 200 electrode holder (screw).
- 4.5m gas hose with quick coupler (female).
- Connector nozzle and feed rolls (V-groove) for 0.6-1.0mm wire
- 3m power cord with plug.
- Solid wire OK AristoRod 12.50 0.8 mm on 200 mm spool.
Electrode ESAB OK 68.81 VacPac
ESAB
Electrode ESAB OK 68.81 VacPac
Art. no.: 81905480
OK 68.81 is a highly alloyed electrode for joint welding of hard welded dissimilar steel, welding of sliding surfaces, and as a buffer layer for welding of hard welded goods. Characteristics of the weldment are high durability, high impact resistance and high wear resistance. The electrode can withstand dilution and dissolving, provides high strength welds in both high alloy and low alloy steel and joint welding of highly dissimilar steel. The high chromium content provides low coefficient of friction and scaling resistance up to 1150oC. Welding at elevated operating temperatures can in many cases be eliminated except for steel with high carbon equivalent, since preheating around 150-200 ° C should be applied. OK 68.81 deserves the term universal electrode for difficult weldments in both common and unusual steel. Suitable applications are rollers, forging tools, thermoforming tools, plastic punch cushions, etc.
Approval: CE, EN 13479, Seproz, UNA 272580
Electrode esab ok 67.70
Art. no.: 122792
OK 67.70 is an over-alloyed stainless steel electrode for welding stainless steel to other types of steel. For welding stainless steel to heat resistant steel, for example SS 2116, SS 2218 ( 10CrMo9-10). At high operational temperatures, OK 92.26 should be used. The electrode is suitable for bottom runs in the shift between compound plates unalloyed and stainless steel. OK 67.70 has excellent welding properties both on direct and alternating current. It can be used in all situations, except vertically downwards, and for all kinds of joins. Current type DC+, AC OCV 55 V.
Code in accordance with: EN 1600 E 23 12 2 L R 3 2. SFA/AWS A5.4 E309MoL-17. Werkstoff No. 1.4459. CSA W48 E309LMo-17.
Approval: CWB CSA W48 - DB 30.039.05 - DNV 309 Mo LR SS/CMn - RINA E 309Mo - Sepros UNA 409820 - VdTÜV 02424 - CL EN 1600 - BV UP- CE EN 13479-
Flowmeter aga rotam plus
AGA
Flowmeter aga rotam plus
Art. no.: 214117
Flow meter, used with flask regulators for argon and argon mixtures, as well as for carbon dioxide, with 3/8" connection on the outlet side. Used in conjunction with regulators with a working pressure manometer graded in bars (eg UNICONTROL 500 argon), the regulator's working pressure should be set to 2.5 bar to provide the correct gas flow. Connects to a T-piece. The T-piece is adjustable to get the right angle in relation to the regulator outlet. T-piece ordered separately. Displays the gas flow in l/min, with a scale rating adjusted for argon and carbon dioxide respectively. The flow is read at the top of the ball / floating body. Supplied with hose connectors for 5.0 mm hoses. Double ROTAM PLUS is used when you want protective gas for both the welding gun and root protection.
Flowmeter aga rotam plus
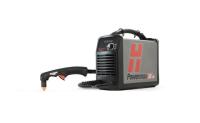
Plasma Cutting Machines Hypertherm Powermax Sync
Hypertherm
Plasma Cutting Machines Hypertherm Powermax Sync
Art. no.: 75295753
**Translation:**

A significantly simplified consumable platform combined with advanced torch communication for automated setup makes Hypertherm’s new Powermax45/65/85/105 SYNC™ plasma systems the smarter choice for all cutting and gouging applications.
Recommended material thickness and cutting speeds:
- **Powermax45 SYNC 400V**: 16mm/500mm per minute. Can handle material thickness up to 29mm without the requirement for cut quality.
- **Powermax65 SYNC**: 20mm/500mm per minute, 25mm/250mm per minute. Can handle material thickness up to 32mm without the requirement for cut quality.
- **Powermax85 SYNC**: 25mm/500mm per minute, 32mm/250mm per minute. Can handle material thickness up to 38mm without the requirement for cut quality.
- **Powermax105 SYNC**: 32mm/500mm per minute, 38mm/250mm per minute. Can handle material thickness up to 50mm without the requirement for cut quality.
Plasma Cutting Machines Hypertherm Powermax Sync
Showing 52 of 512